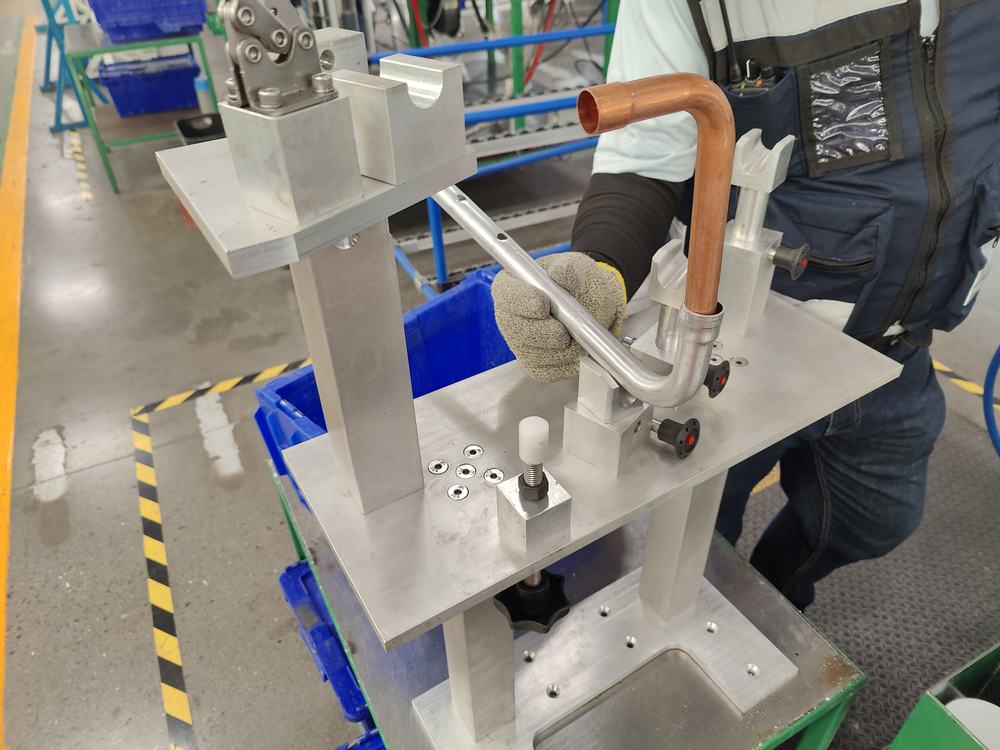
Fixture for automated brazing
Automated brazing station with a flexible design: one fixture runs seven part numbers instead of seven separate fixtures.
Holding, assembly, inspection and material-handling fixtures. We design the fixture from your drawing, your sample part or the problem on your line.
Same-day reply during plant hours · Monday to Friday, 9 a.m. to 6 p.m. (Monterrey time, CST) · +52 81 8706 7945
Automated brazing station with a flexible design: one fixture runs seven part numbers instead of seven separate fixtures.
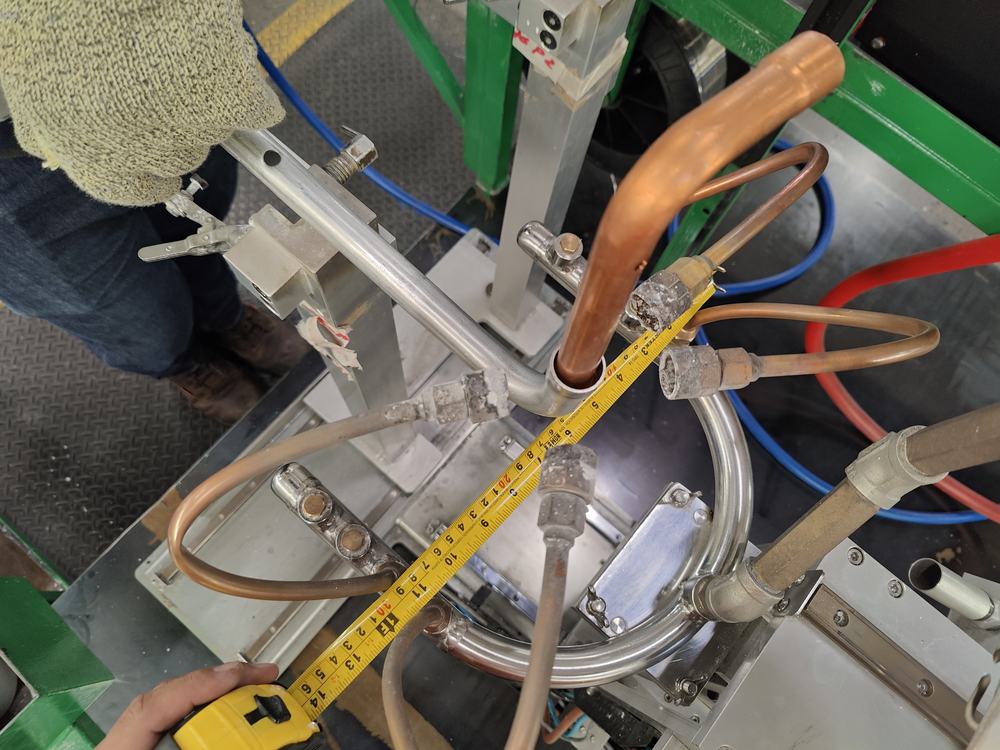
The checking fixture holds the part and is also used to measure it. One operation instead of two.
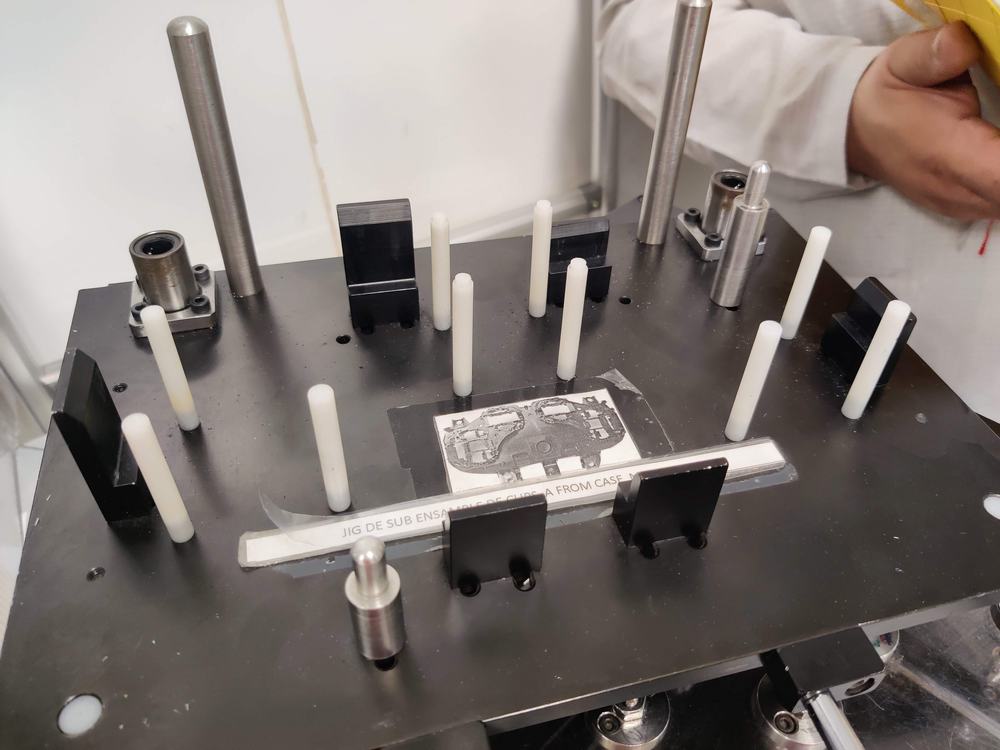
Locating pins to position and check components before assembly.
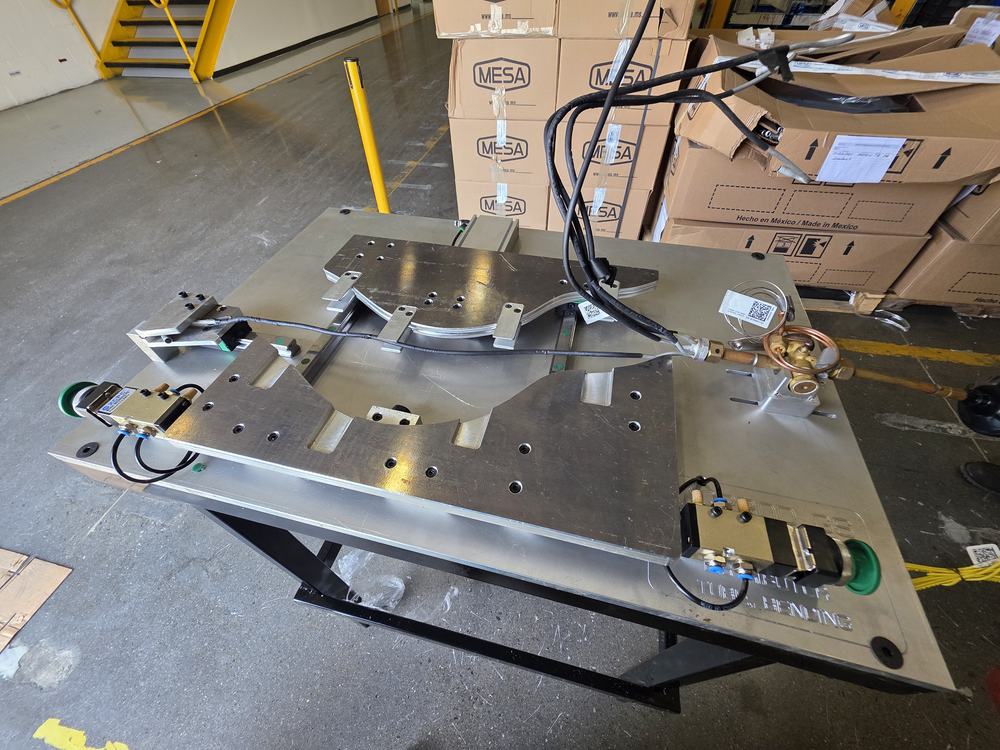
Holding and tube forming in a single station, installed on the customer's line.
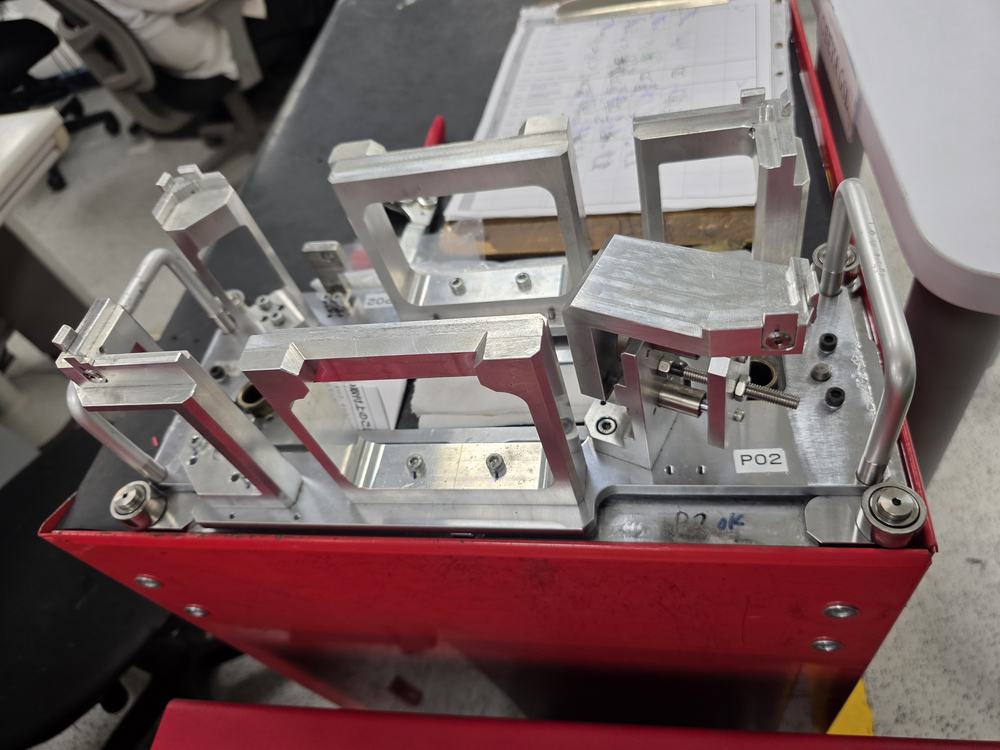
A set mounted on a line cart to cover several operations on the same model.
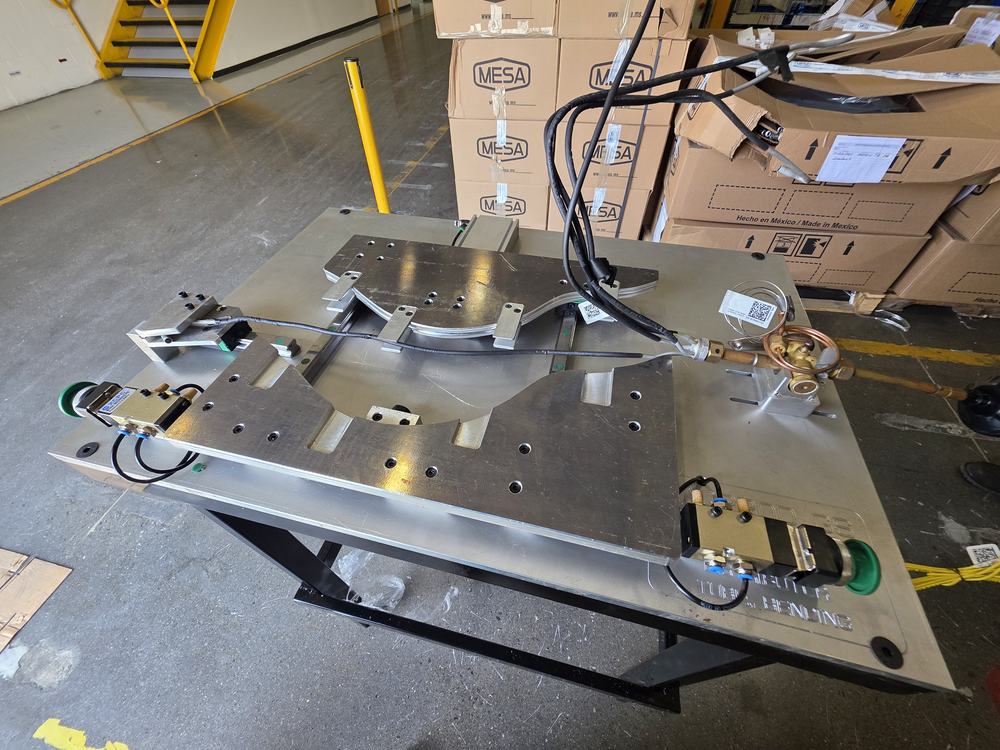
Power-assisted clamping for repeatable assembly, located on the 3-2-1 principle.
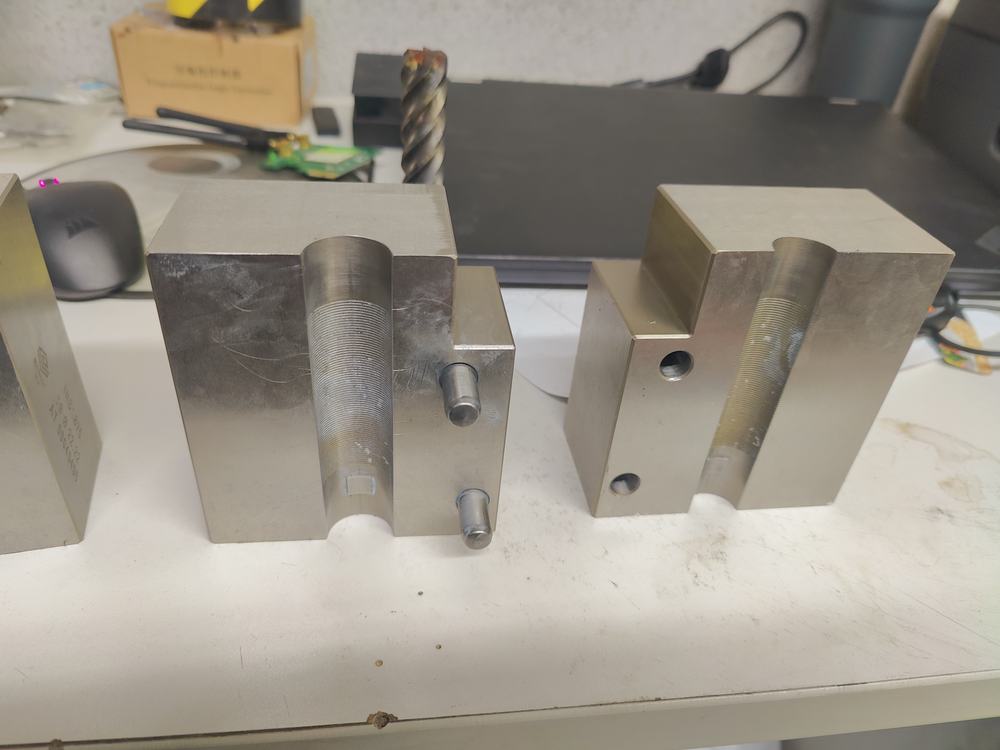
The fixture components are machined right here, not bought from a catalog.
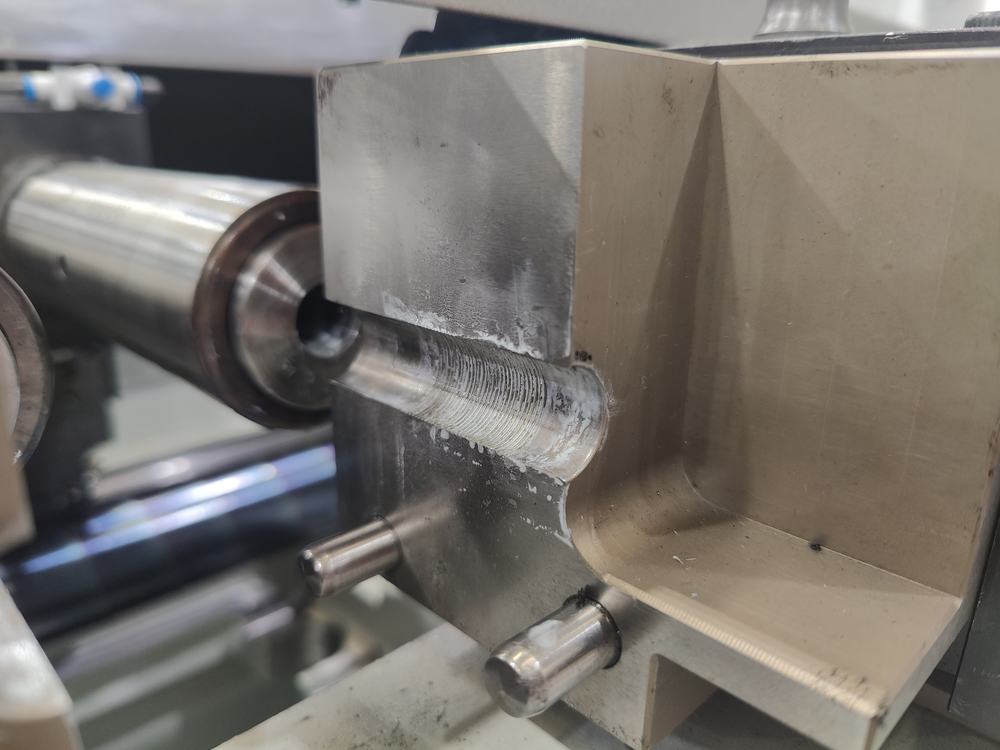
Turned and ground components for the fixture itself or for the customer's machine.
Every part needs six points of contact to be fully constrained. That is the starting point for every fixture that leaves this plant.
Because it is the difference between a fixture that repeats and one that only holds. Every fixture we deliver starts from a defined locating scheme, not from adding clamps until the part stops moving.
The questions that come up on the first call. If yours isn't here, send it by WhatsApp.
No. We work from a drawing, a STEP file, a photo of the part or the physical sample part. A description of the problem on your line is also enough to start.
PDF, DWG and STEP. Send them by WhatsApp to +52 81 8706 7945 or attach them to an email to ventas@maquinadosyproductos.com.
Every fixture starts from the 3-2-1 locating principle: three supports on the primary plane seat the part, two on the secondary plane align it and one on the tertiary plane locks it in place. Six points of contact, zero degrees of freedom. That is the difference between a fixture that repeats and one that only holds the part.
No. The components are machined in our plant, not bought from a catalog. That lets us design the fixture around your part instead of fitting the part to whatever was available.
Yes, and we recommend it when the operation allows. A fixture that holds the part and is also used to measure it turns two operations into one.
Yes. A checking fixture is an inspection fixture: it holds the part in its datum position so you can measure critical dimensions or check geometry with go/no-go gauges. We design it from the part drawing and machine it in the same plant in Monterrey.
We reply with scope and lead time within one business day. During plant hours, Monday to Friday, 9 a.m. to 6 p.m. (Monterrey time, CST), the reply usually comes the same day.
A drawing, a STEP file, a photo or the sample part. We reply with scope and lead time within one business day.